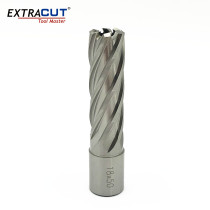
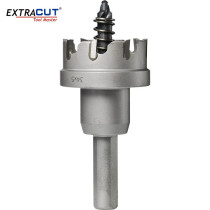
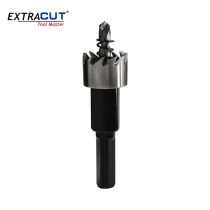
EXTRACUT T.C.T. Annular Cutters (also known as core drills or magnetic drill cutters) designed for high-efficiency hole making in structural steel, I-beams, channels, and thick plate using magnetic base drilling machines. Unlike twist drills that remove 100% of the material, annular cutters only remove the periphery of the hole, cutting faster with less power consumption and producing a solid core that can be reused.
Key Features
- Annular Cutting Principle — Removes only the outer ring of material, reducing cutting force by up to 60% compared to solid twist drills while producing a reusable solid core.
- T.C.T. Tip Configuration — Multiple precision-ground tungsten carbide tips distributed evenly around the cutting circumference ensure balanced cutting forces and consistent tool life.
- Weldon Shank Design — Standard Weldon flat-shank mounting provides maximum torque transmission and quick-change compatibility with all major magnetic drill brands.
- Pilot Pin System — Included center pilot pin ensures accurate hole positioning and acts as a coolant feed channel for through-hole applications.
- Dual Flute Geometry — Twin spiral flutes provide efficient chip evacuation even at full depth, preventing chip packing and tool binding.
- Heat-Treated Body — Through-hardened alloy steel body (42-45 HRC) resists deflection and maintains concentricity under heavy cutting loads.
Applications
Widely used in steel fabrication, bridge construction, shipbuilding, heavy equipment manufacturing, structural steel erection, railway maintenance, and on-site machining where magnetic base drills are employed. Suitable for creating holes in I-beams, H-columns, channel iron, angle iron, flat bar, and round tube with thicknesses from 10mm to 100mm.
Specifications
| Specification |
Value |
| Diameter Range |
Ø12mm – Ø100mm (1/2" – 4") |
| Cutting Depth |
25mm / 35mm / 55mm / 75mm / 110mm |
| Shank Type |
Weldon Shank (19mm / 3/4") |
| Body Material |
Alloy Steel (42-45 HRC) |
| Tip Material |
Tungsten Carbide (YG8 Grade) |
| Number of Teeth |
4 – 12 (varies by diameter) |
| Cutting Speed |
20 – 35 m/min (structural steel) |
| Feed Rate |
0.04 – 0.12 mm/tooth |
| Coolant Method |
Internal / External Coolant Through |
| Machine Compatibility |
All Magnetic Base Drills (BDS/ALFRA/HMT/etc.) |