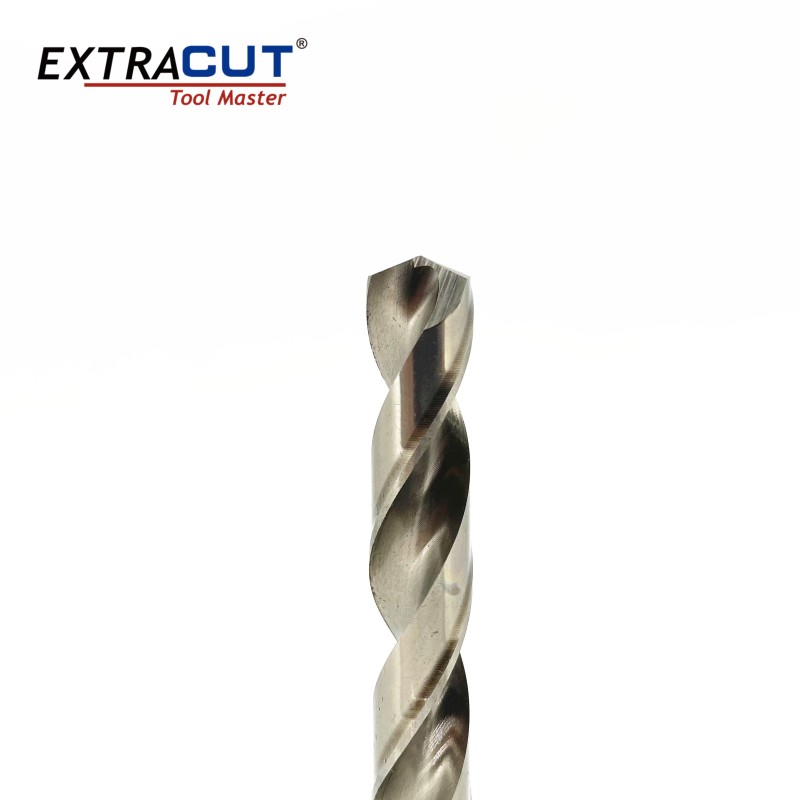
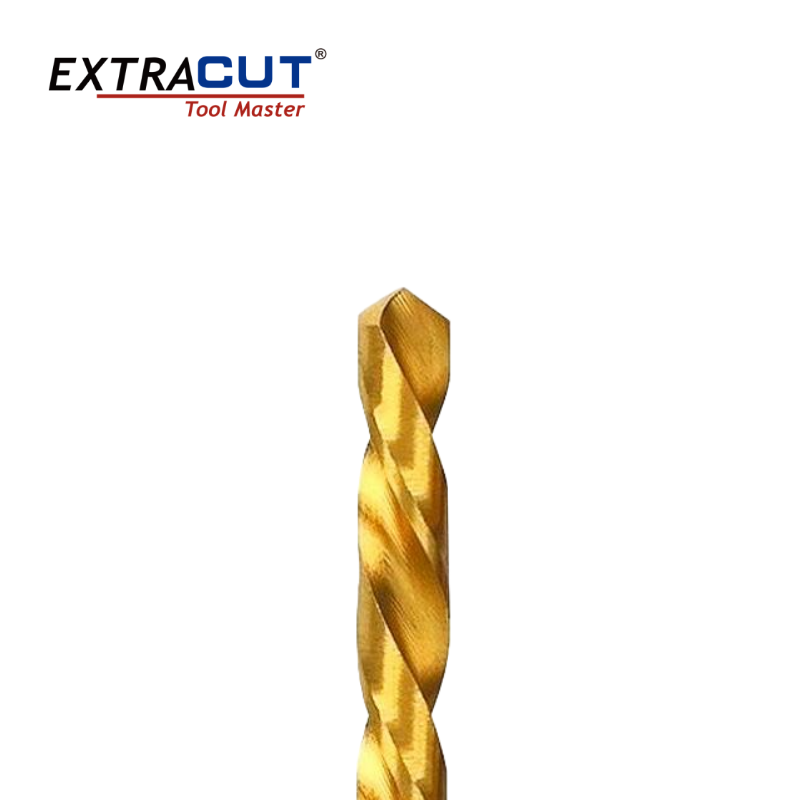
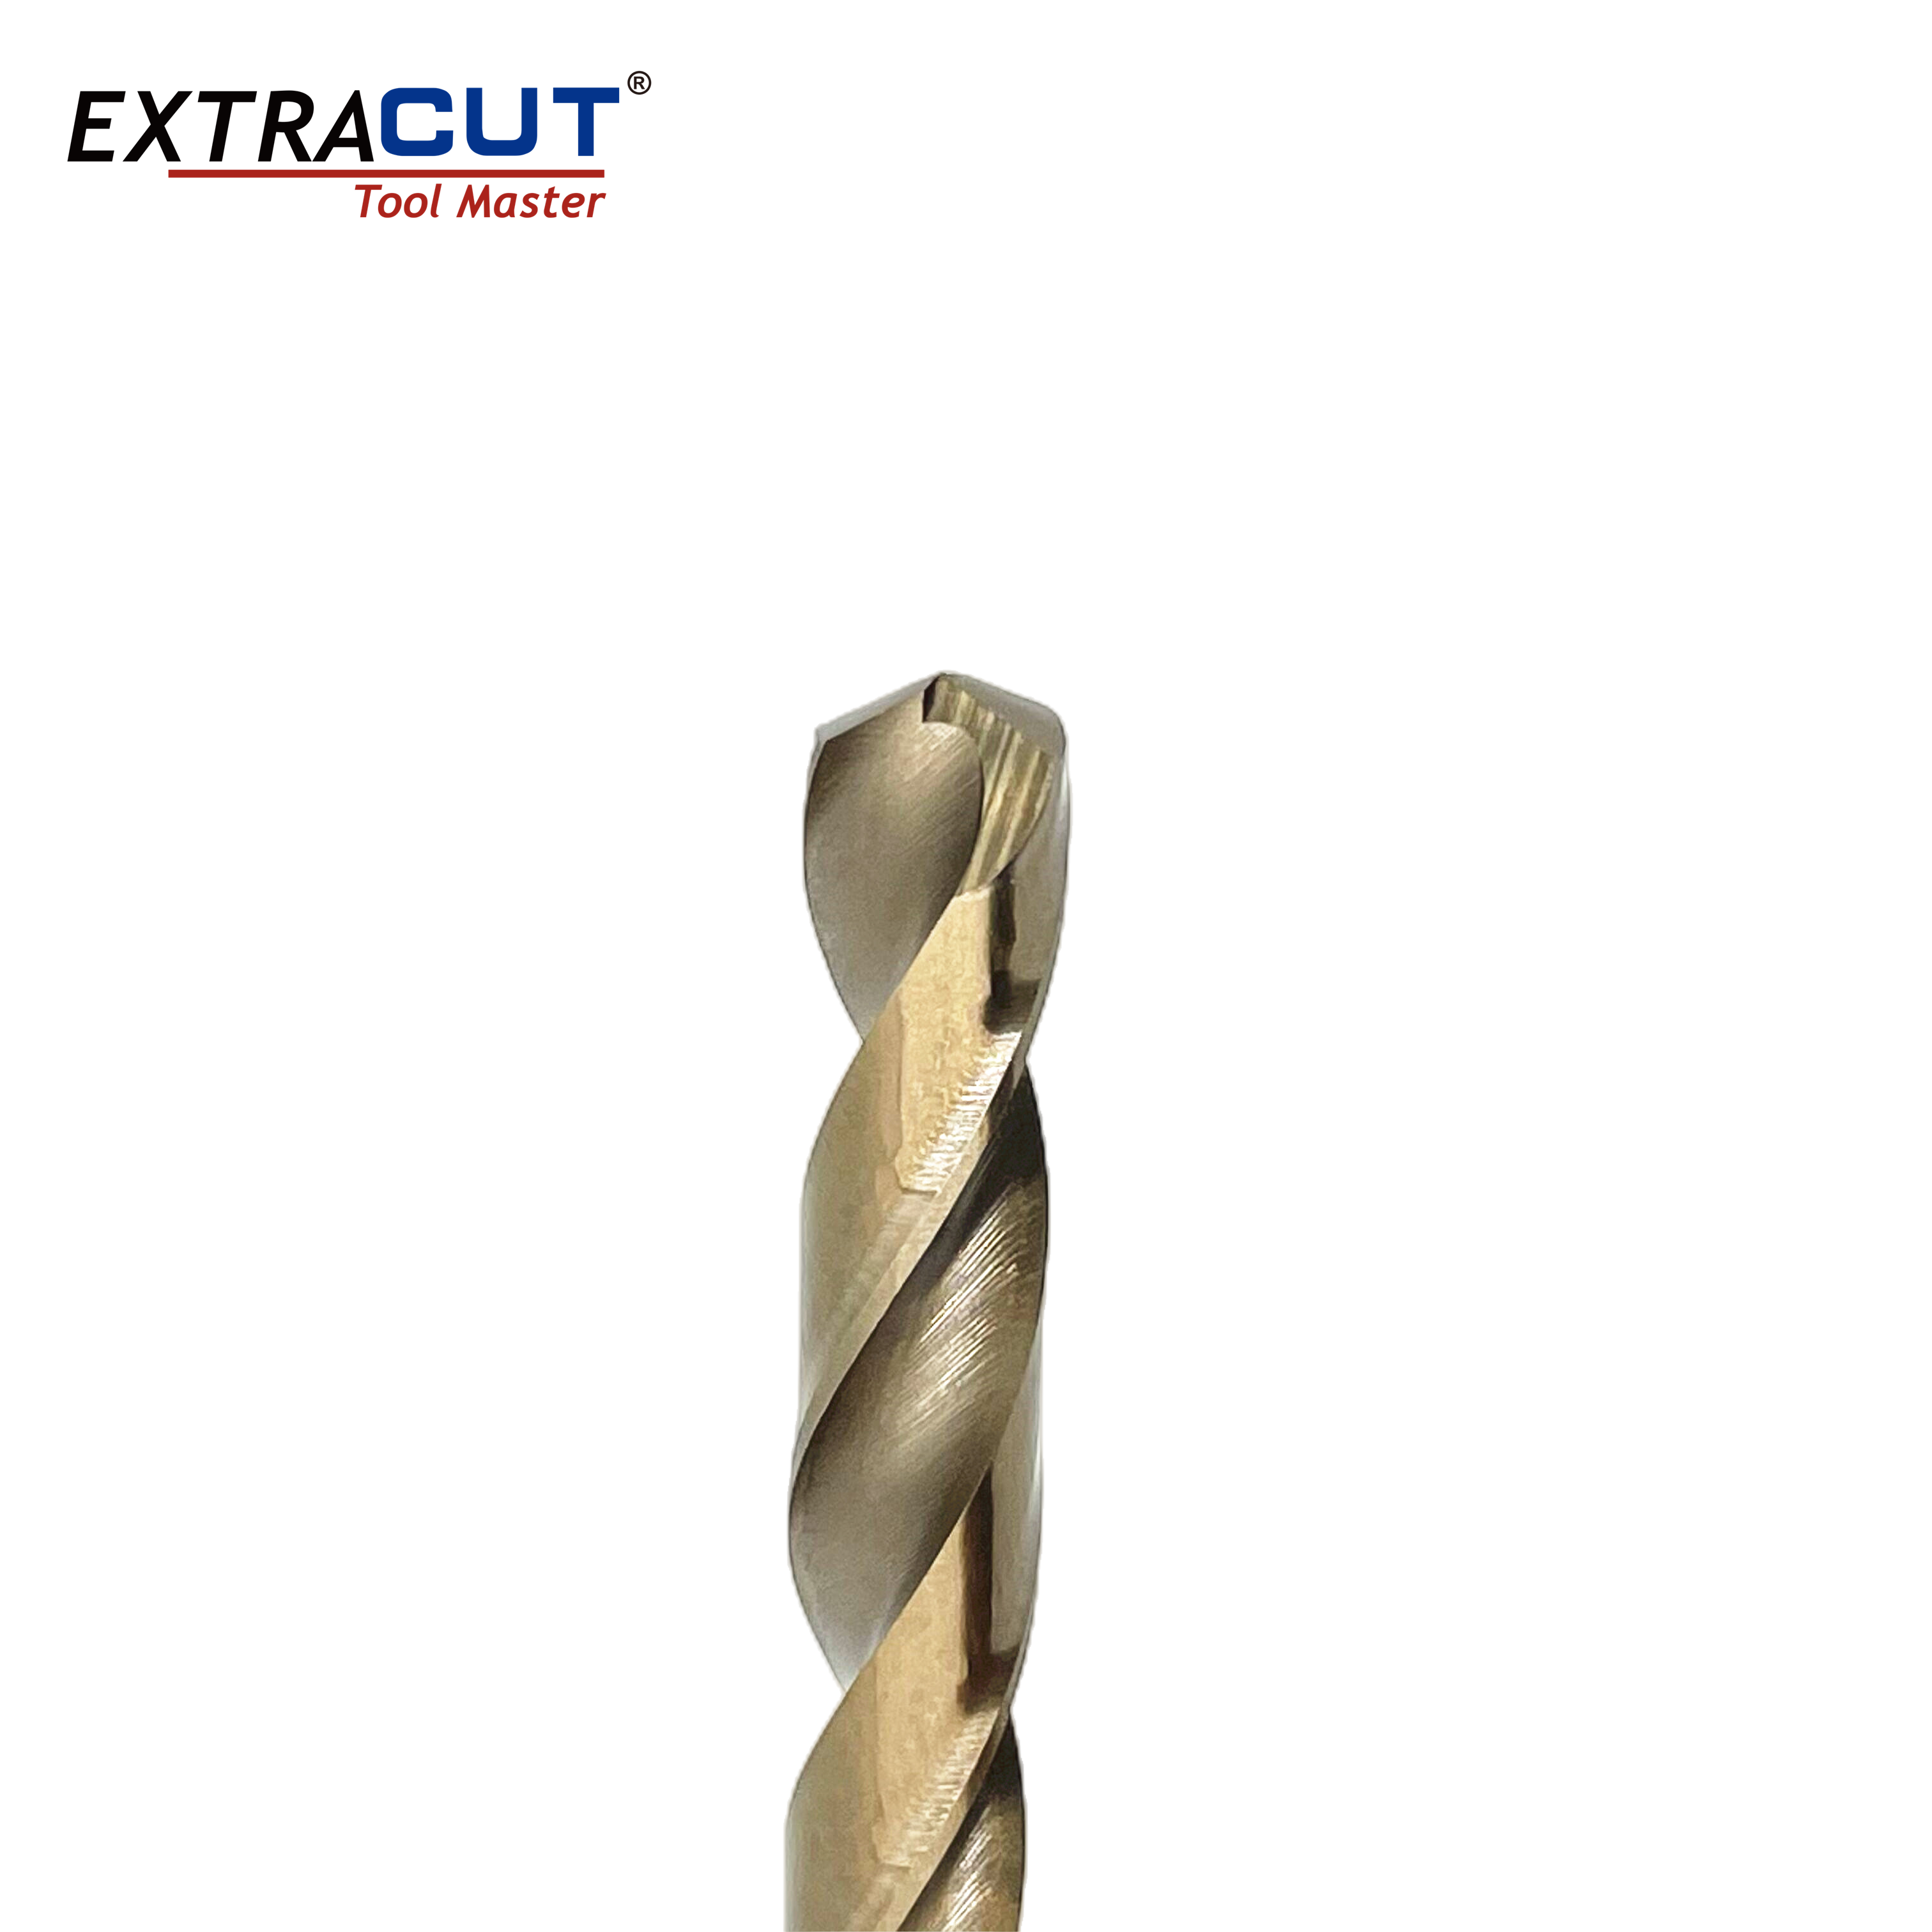
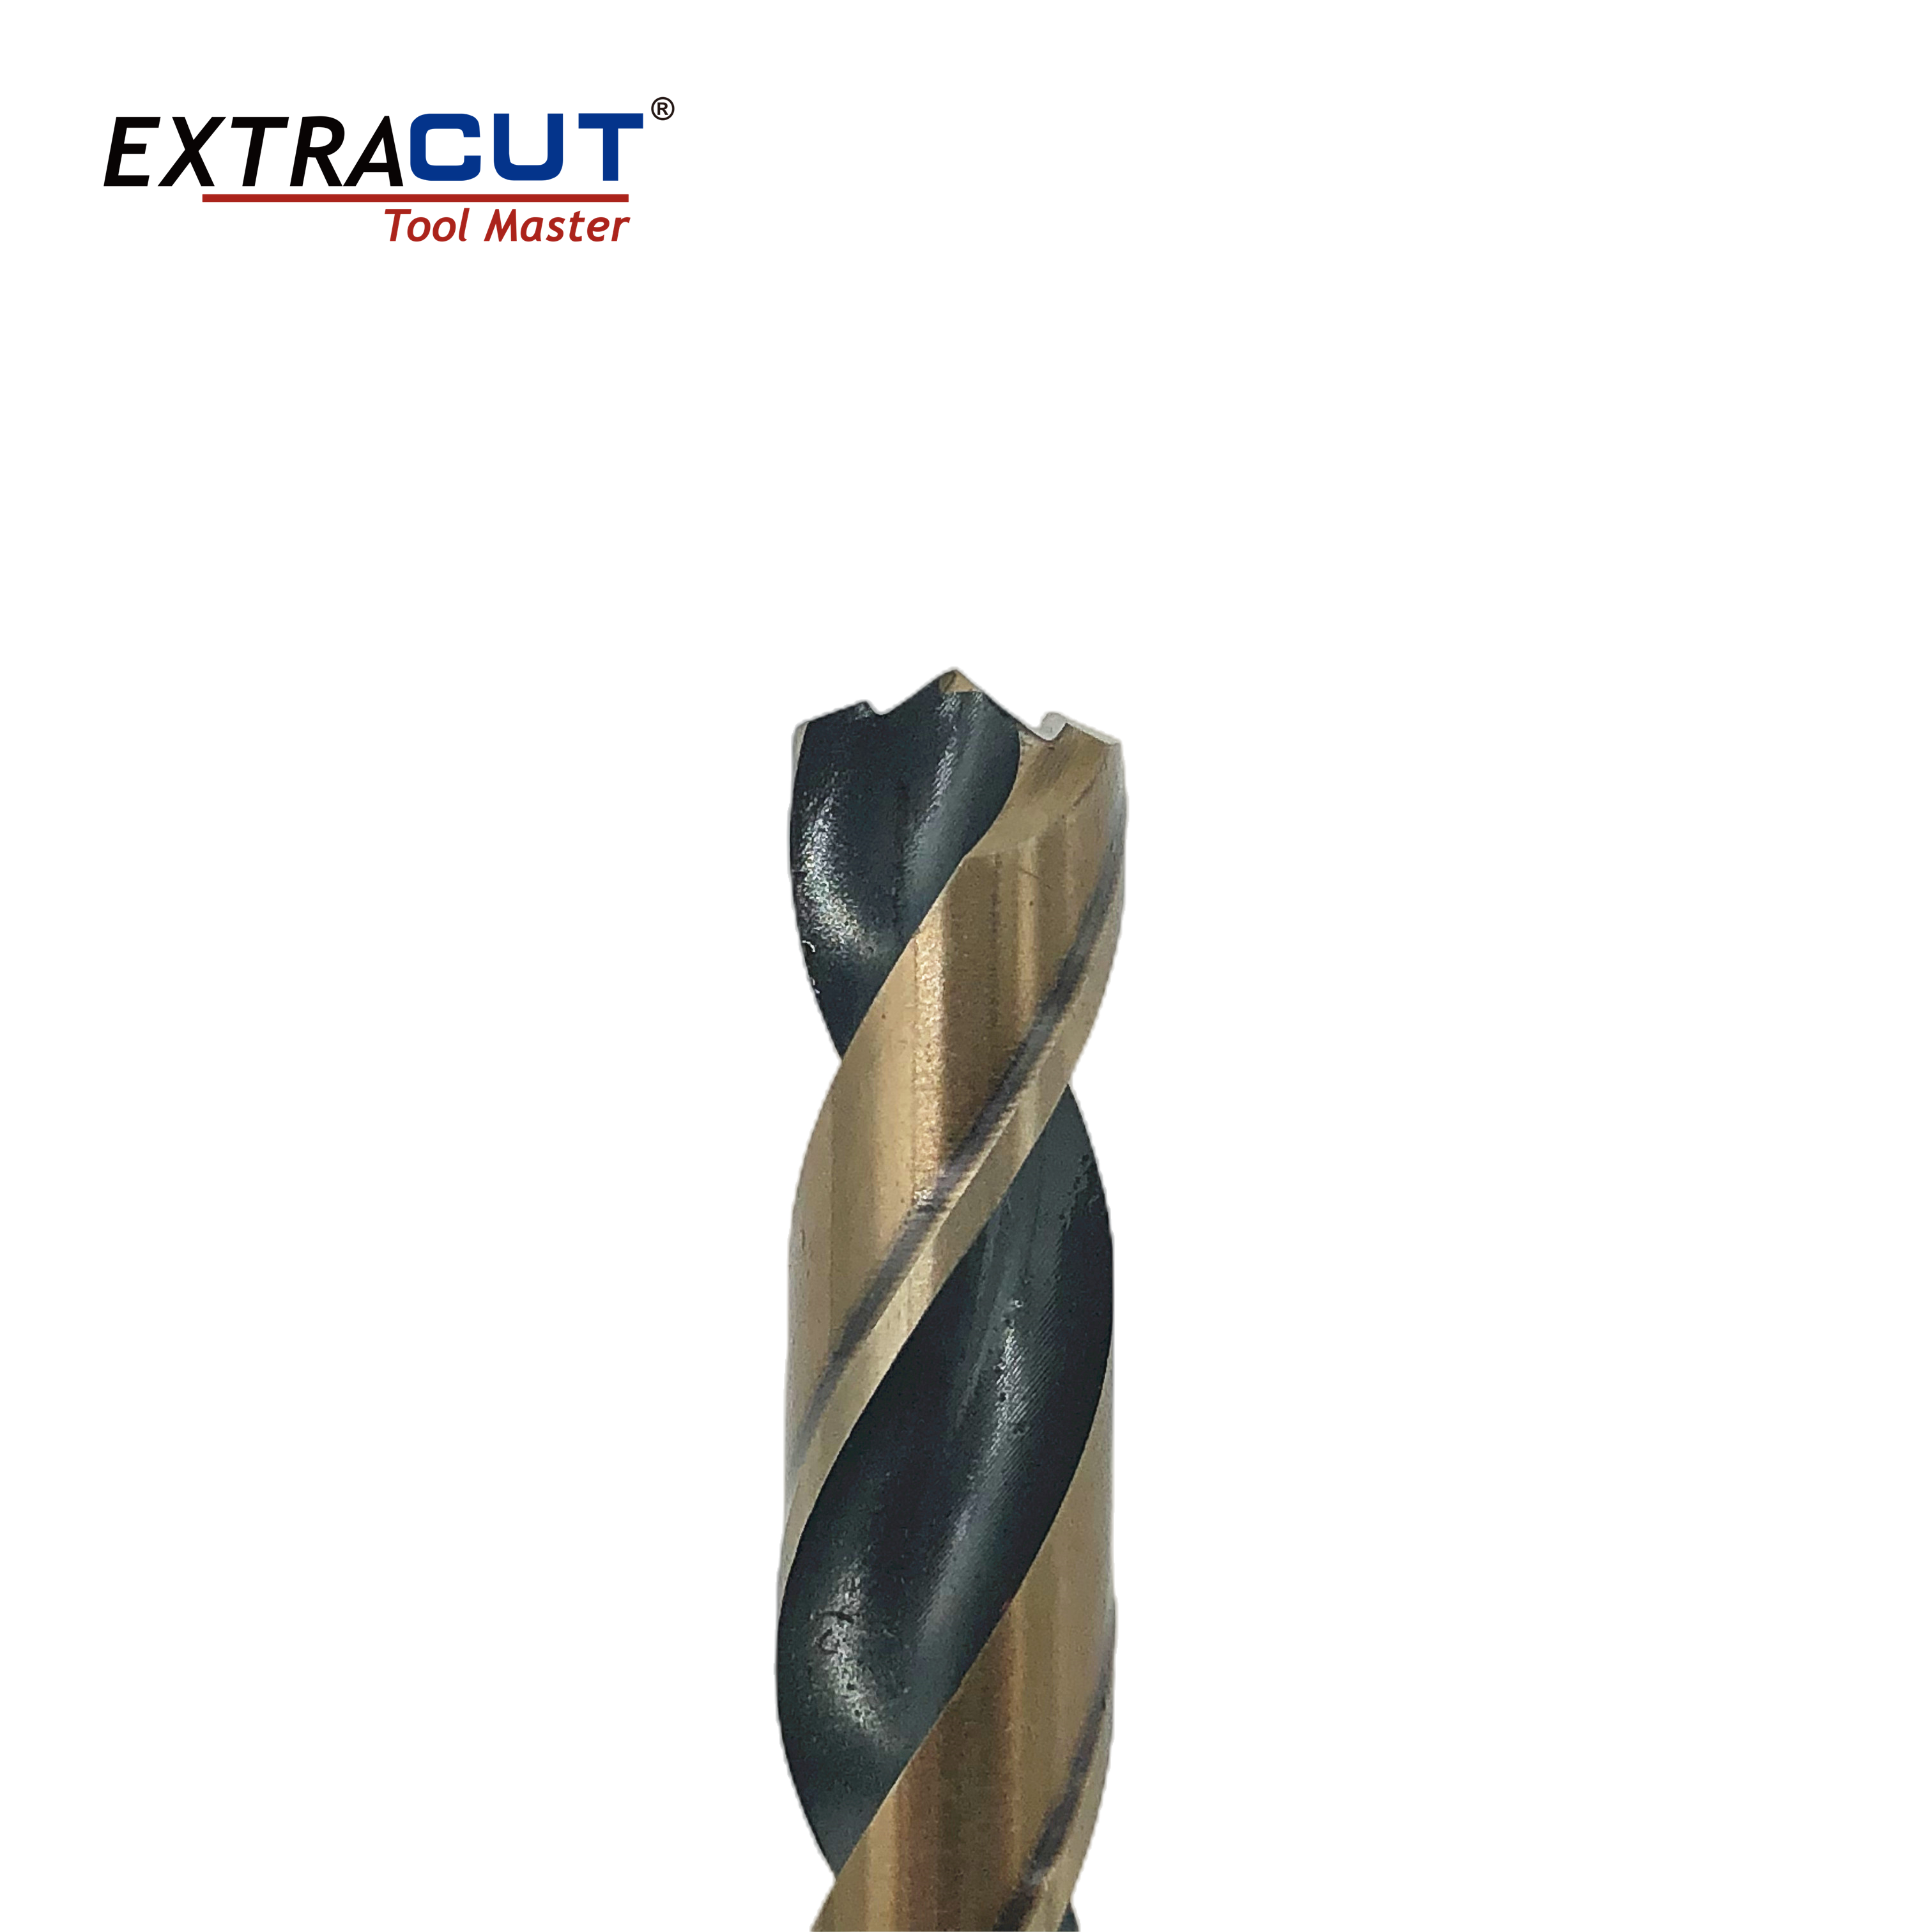
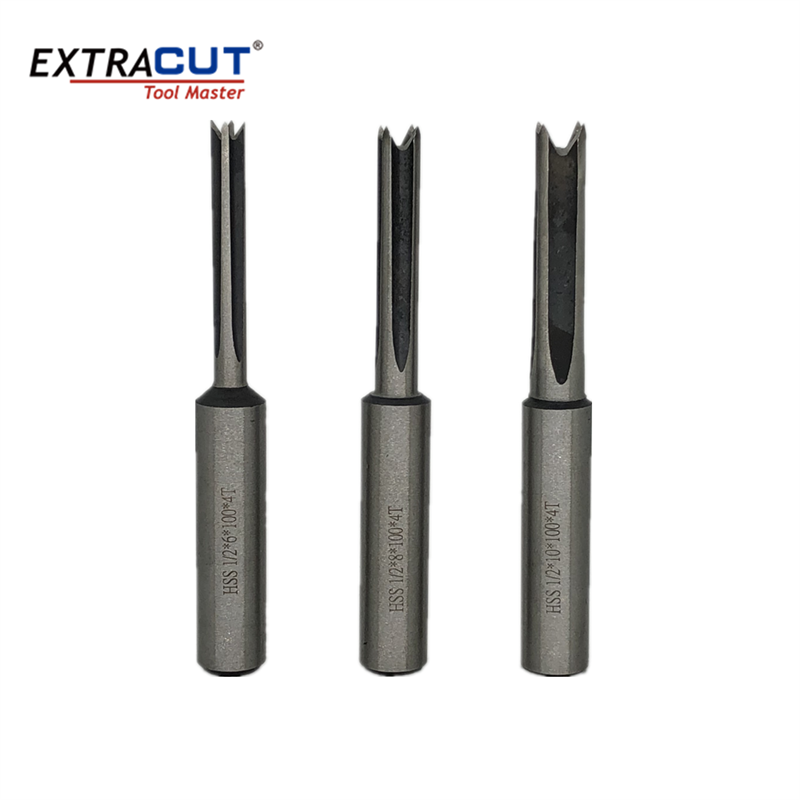
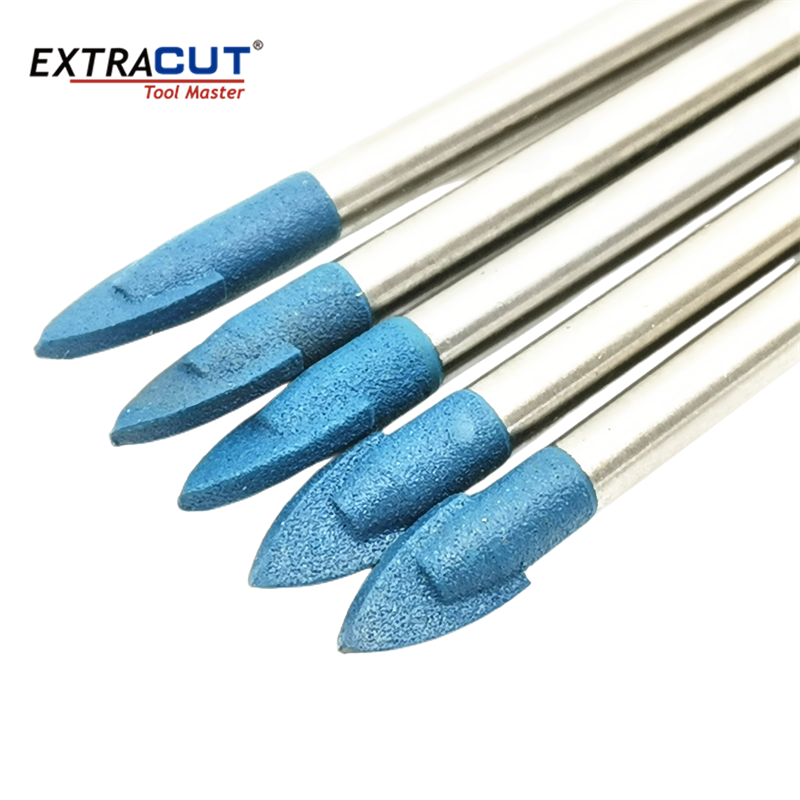
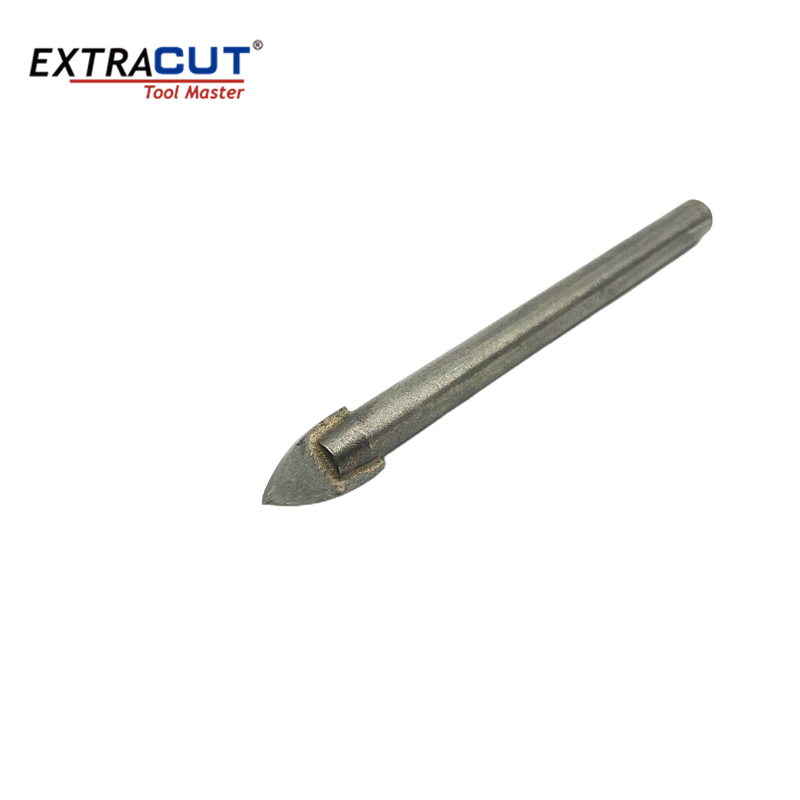
EXTRACUT HSS Bullet Tip (Dwelling) Drill Bits a specialized bullet-nose point geometry designed specifically for drilling thin sheet metal and tubing without tearing, burring, or deforming the material. The unique tip shape allows the drill to "dwell" momentarily before cutting, creating a clean shearing action rather than the punching effect of conventional twist drills on thin materials.
Key Features
- Bullet-Nose Point Geometry — Rounded bullet-shaped tip shears material cleanly rather than punching through, eliminating burrs and tear-out on thin-gauge materials down to 0.5mm thickness.
- Zero Burr Formation — Shearing cutting action produces clean hole edges on both entry and exit sides — no deburring required for most applications.
- Thin Material Specialist — Engineered for optimal performance on sheet metal thicknesses from 0.5mm to 3mm where standard drills cause deformation.
- Self-Centering Design — Bullet tip naturally centers itself on marked points, eliminating the need for center punching on thin sheets.
- Reduced Thrust Force — Geometry requires 40–60% less axial thrust than conventional 118° point drills, preventing material buckling.
- Extended Tool Life — Lower cutting forces and reduced heat generation extend tool life significantly in thin-material applications.
Applications
Sheet metal fabrication (steel, aluminum, stainless steel panels 0.5–3mm thick), HVAC ductwork, electrical enclosure manufacturing, automotive body panel drilling, aircraft skin drilling, appliance manufacturing, and any application requiring clean, burr-free holes in thin-gauge materials without backup support.
Specifications
| Specification |
Value |
| Material |
M2 HSS (Standard) / M35 Co (Optional) |
| Point Type |
Bullet Nose (Dwelling Point) |
| Optimal Thickness |
0.5mm – 3.0mm (thin sheet/tubing) |
| Diameter Range |
Ø3mm – Ø16mm |
| Thrust Reduction |
40% – 60% vs 118° point |
| Burr Formation |
Minimal to None |
| Hole Quality |
Clean shear, no tear-out |
| Center Punch Required |
No (self-centering) |
| Cutting Speed (Steel) |
25 – 40 m/min |
| Cutting Speed (Aluminum) |
80 – 120 m/min |
| Backup Support |
Not required (unlike standard drills) |